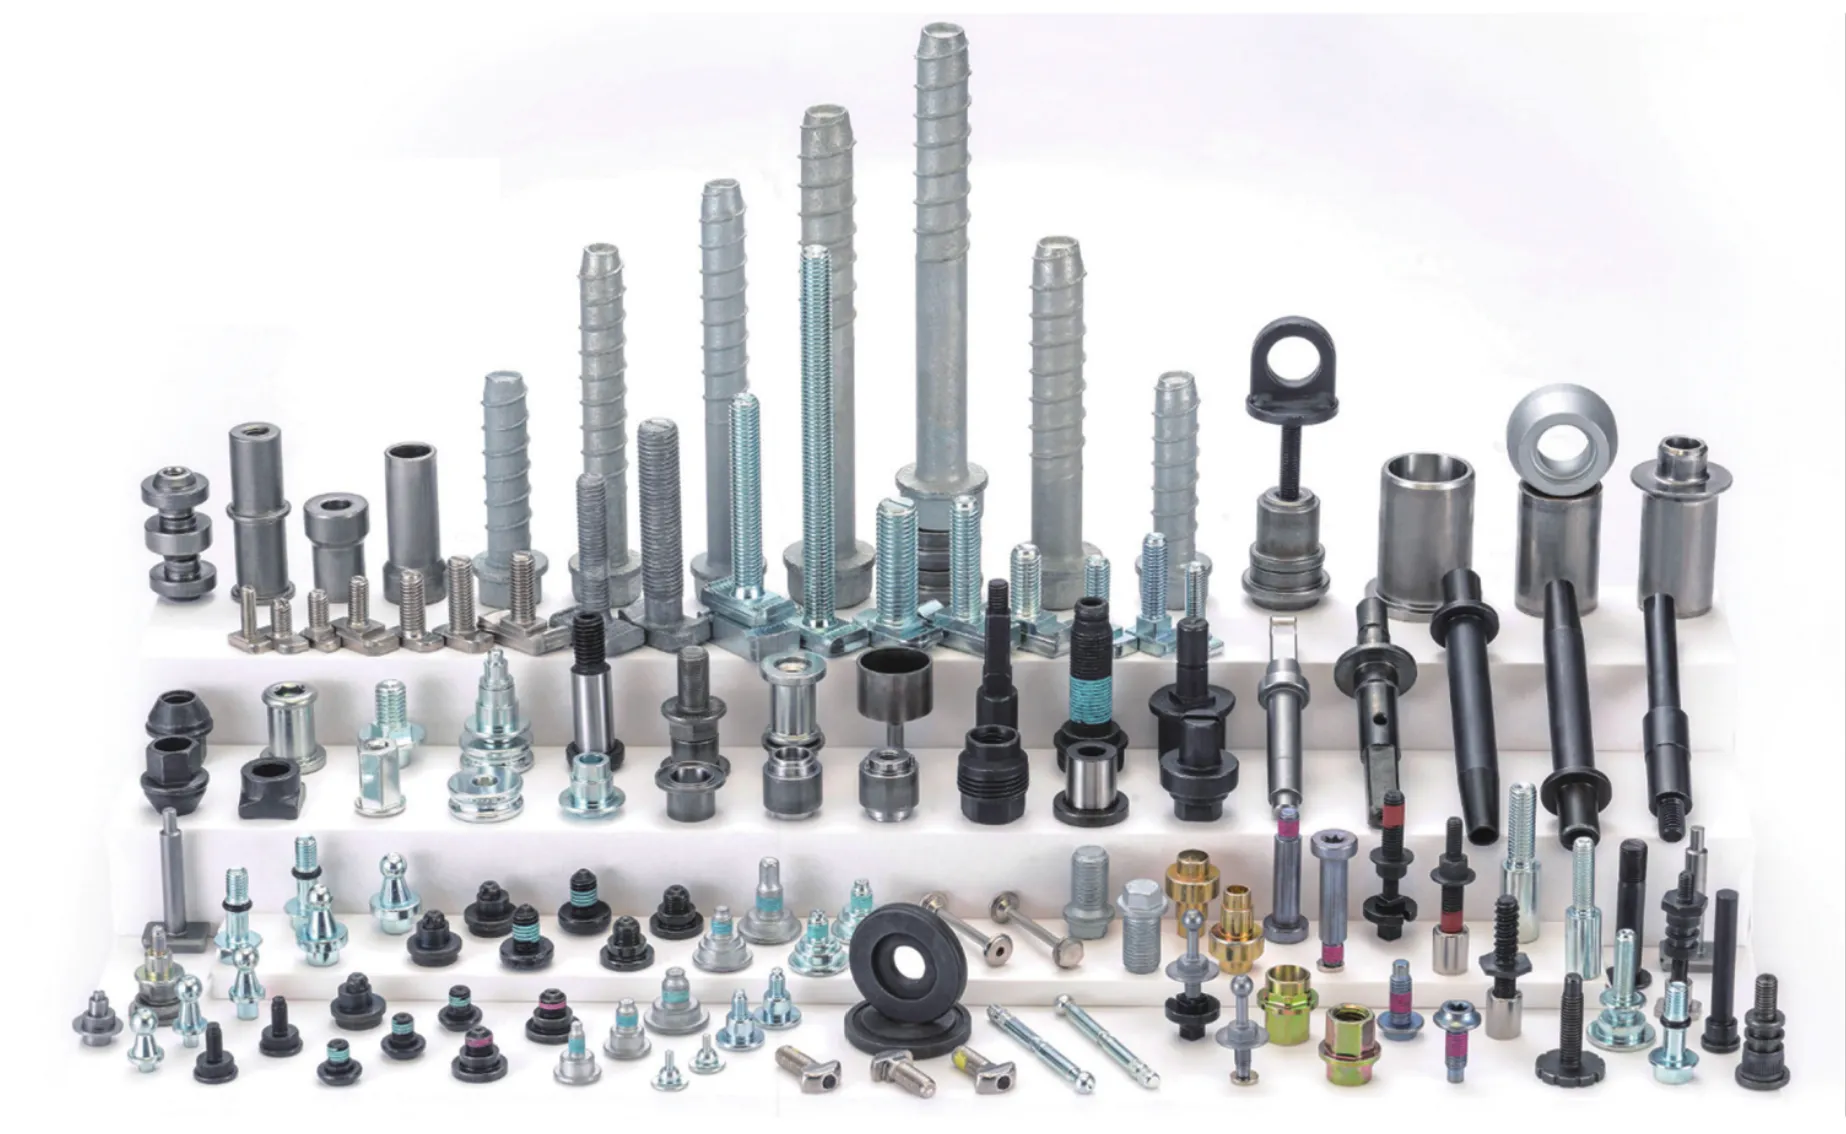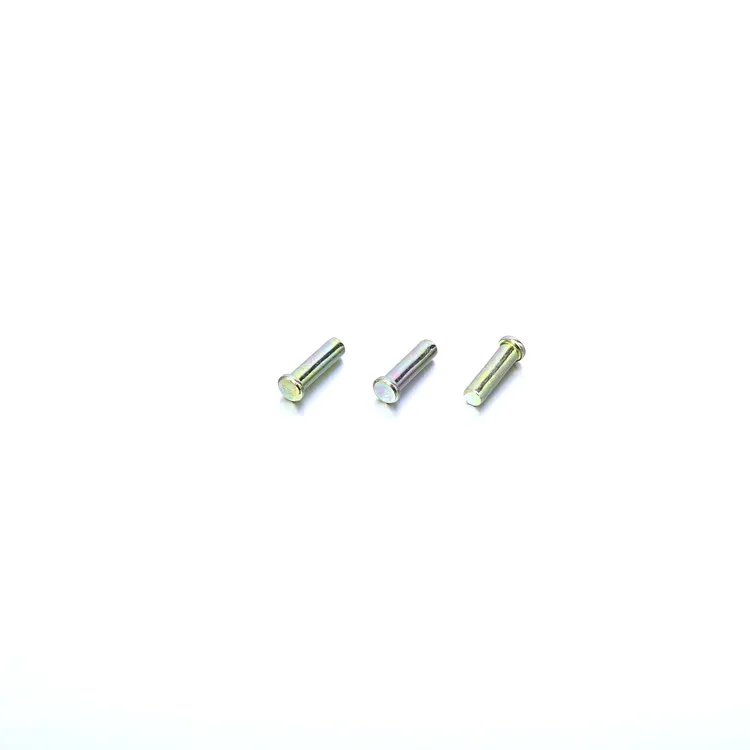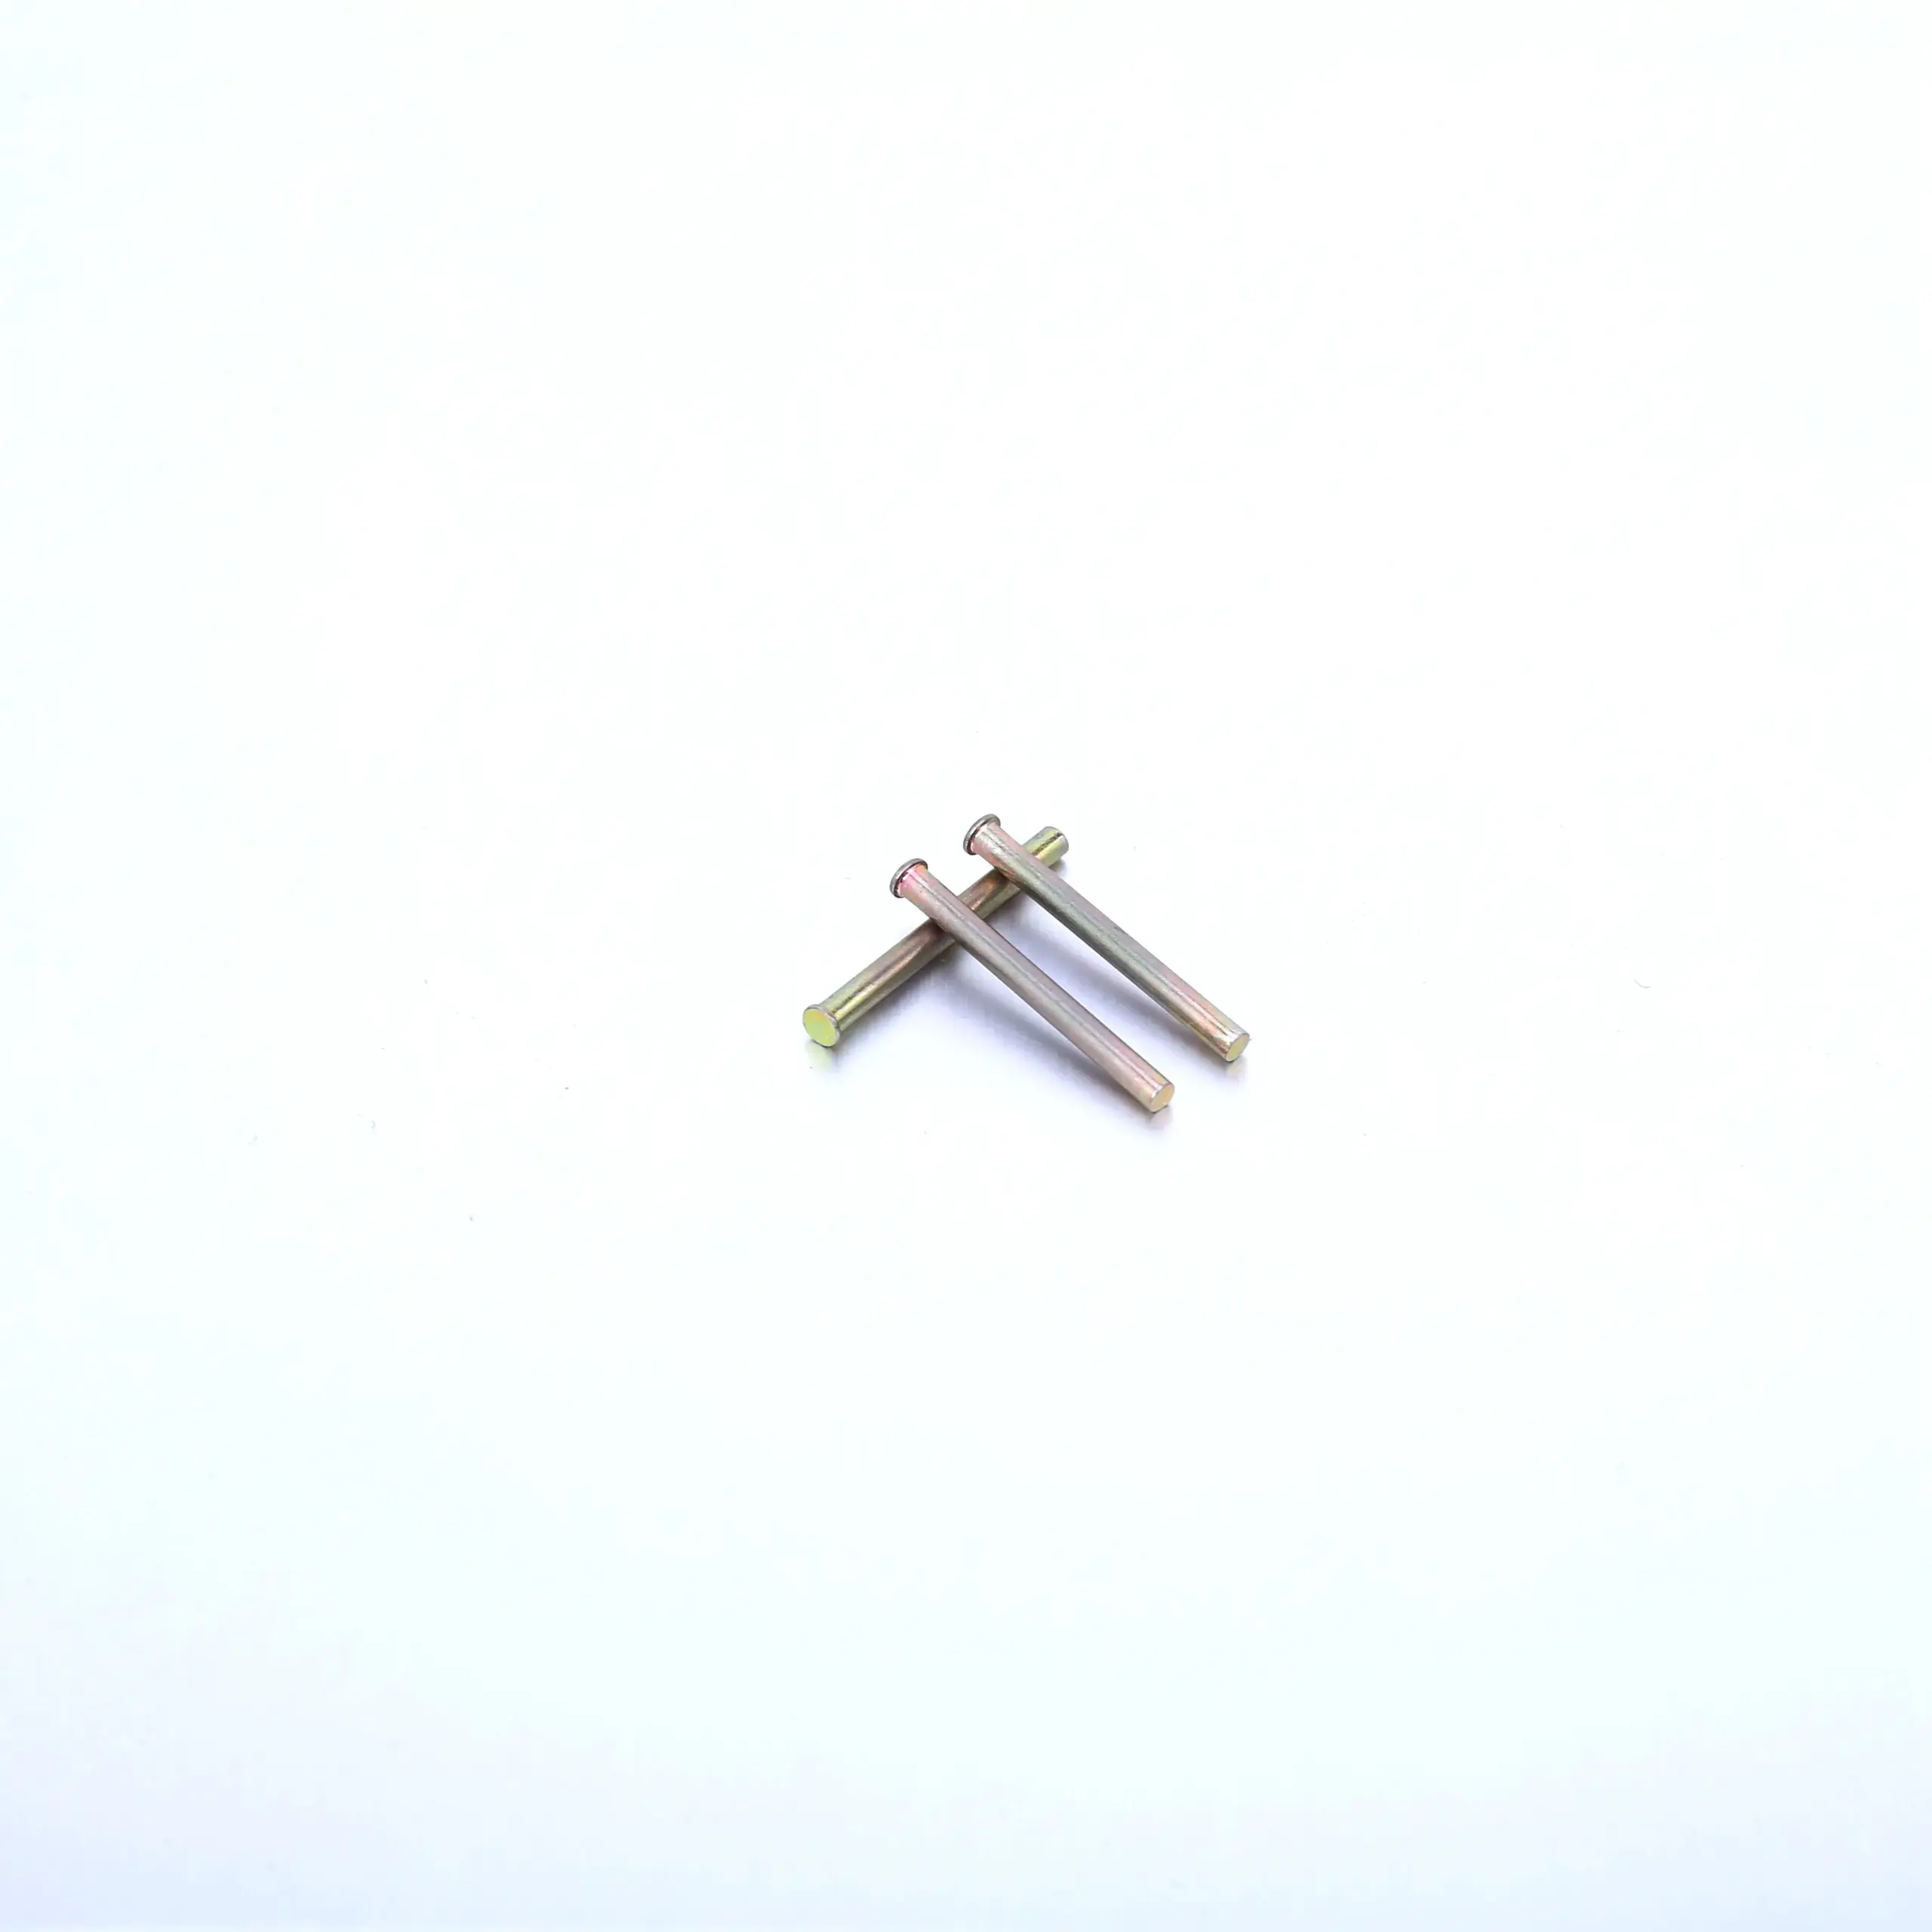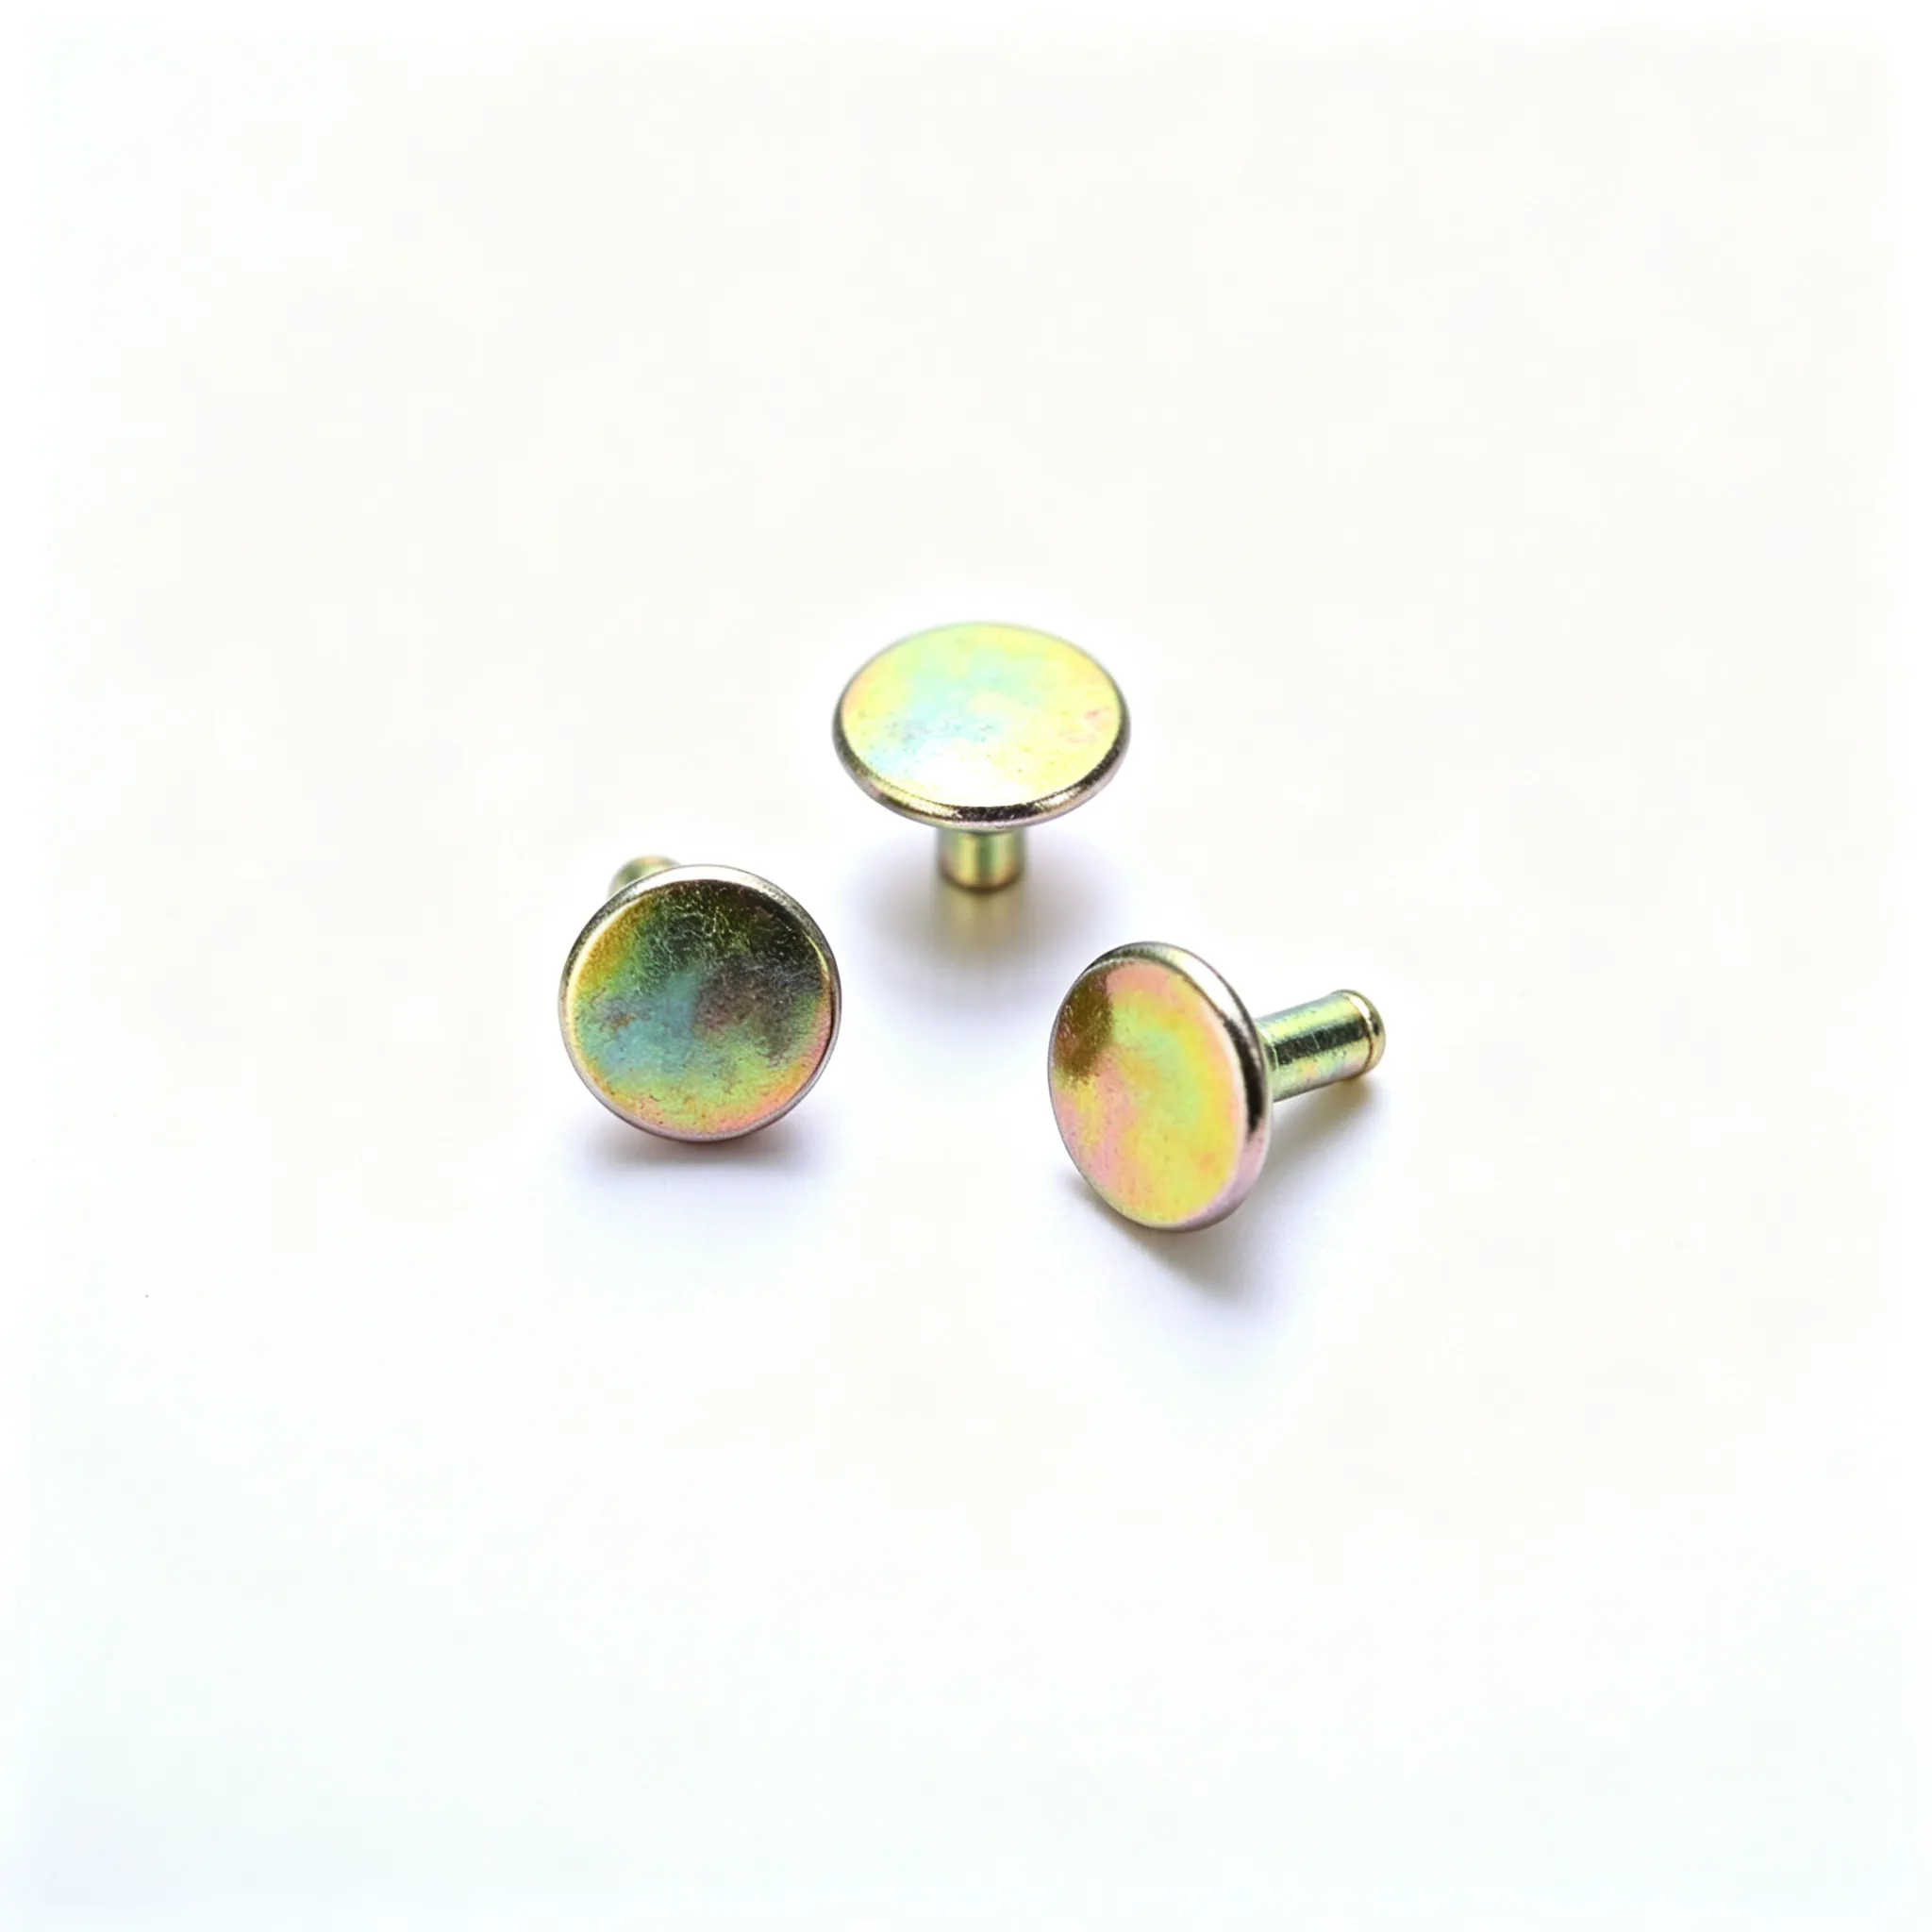
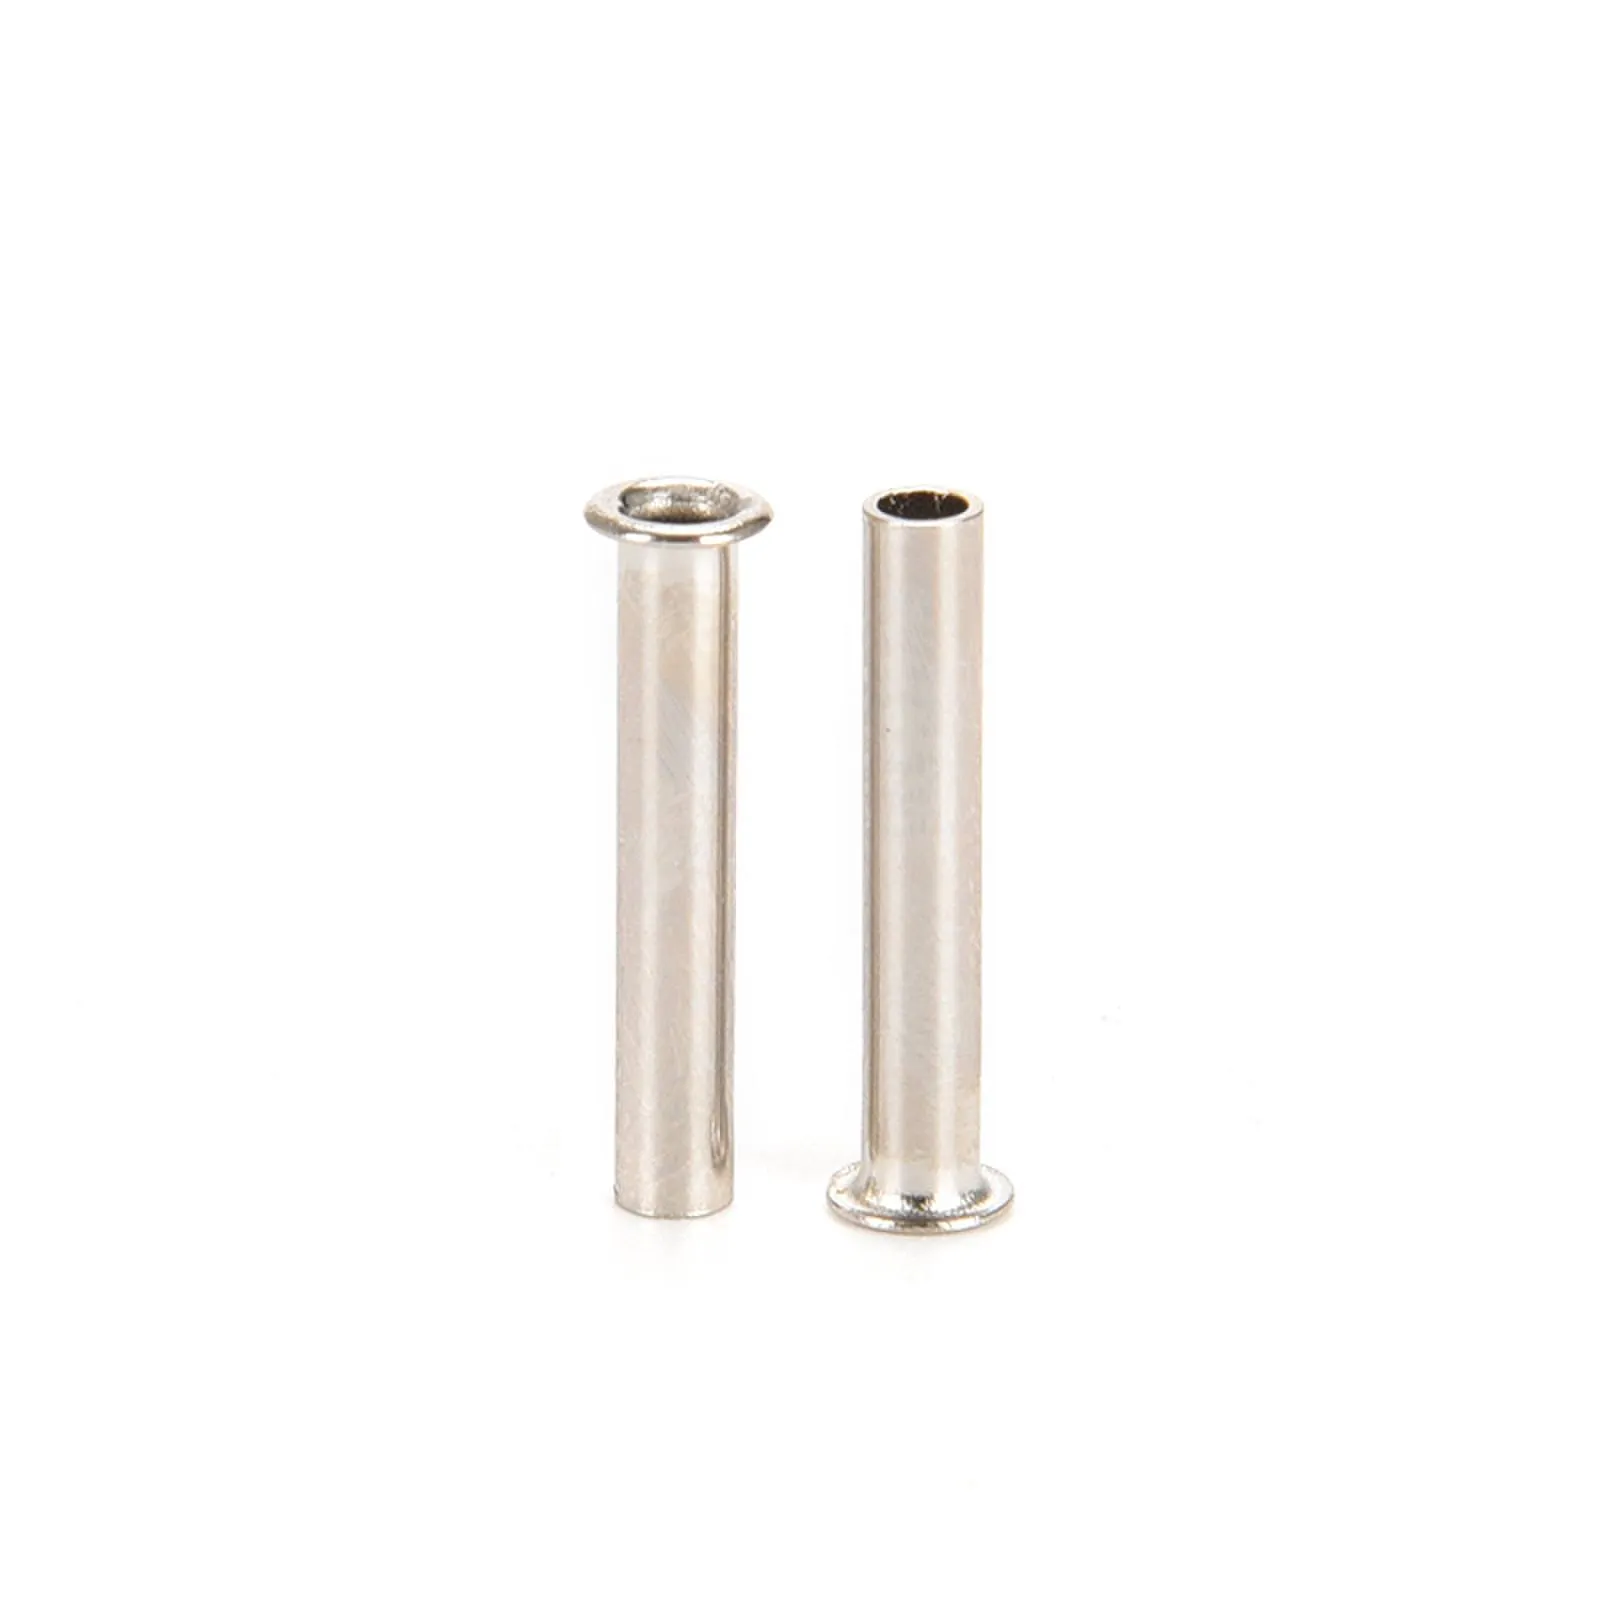
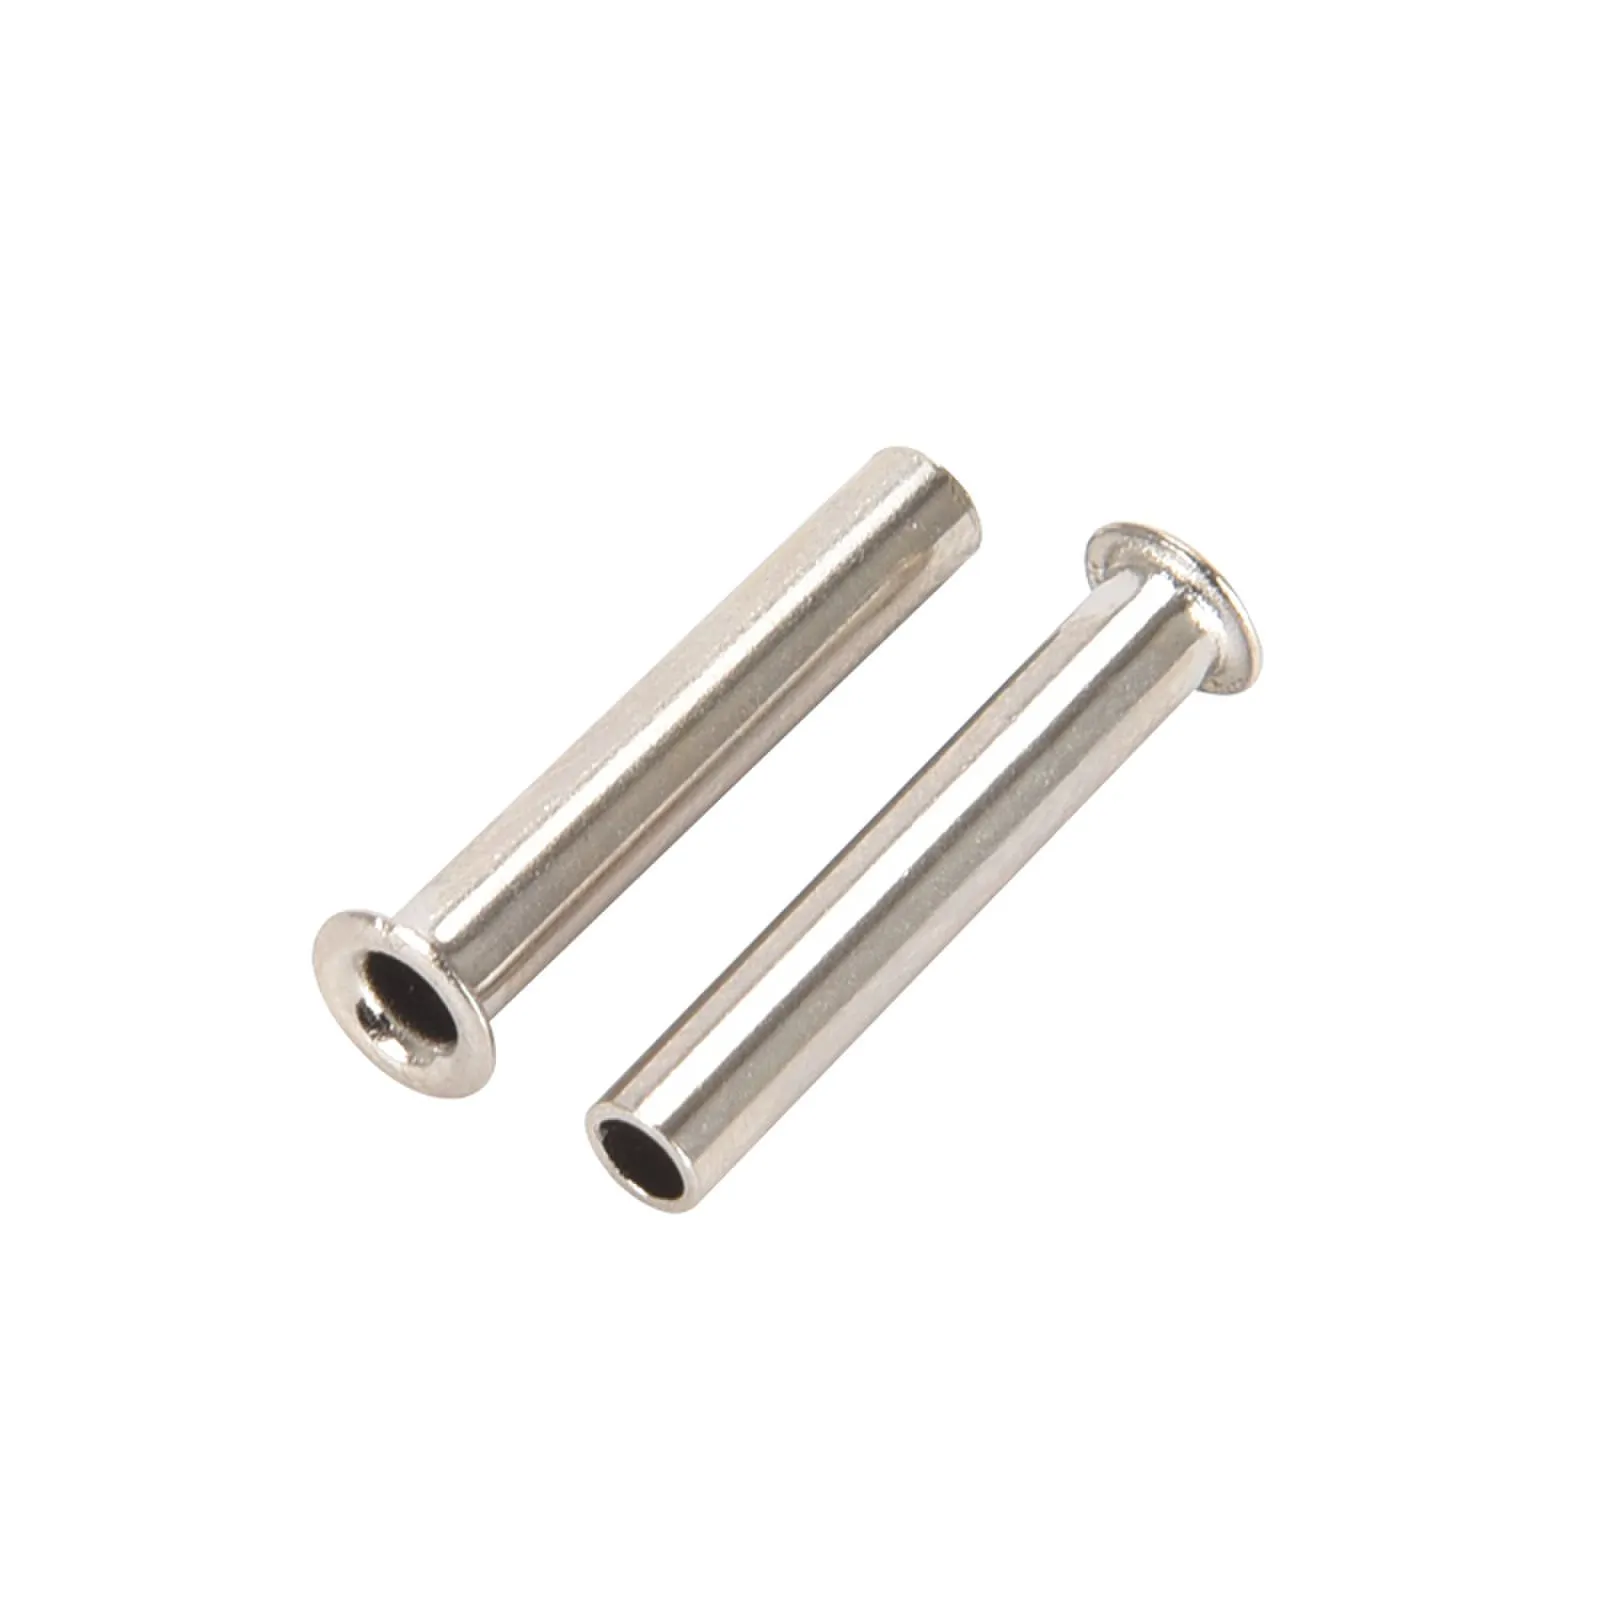
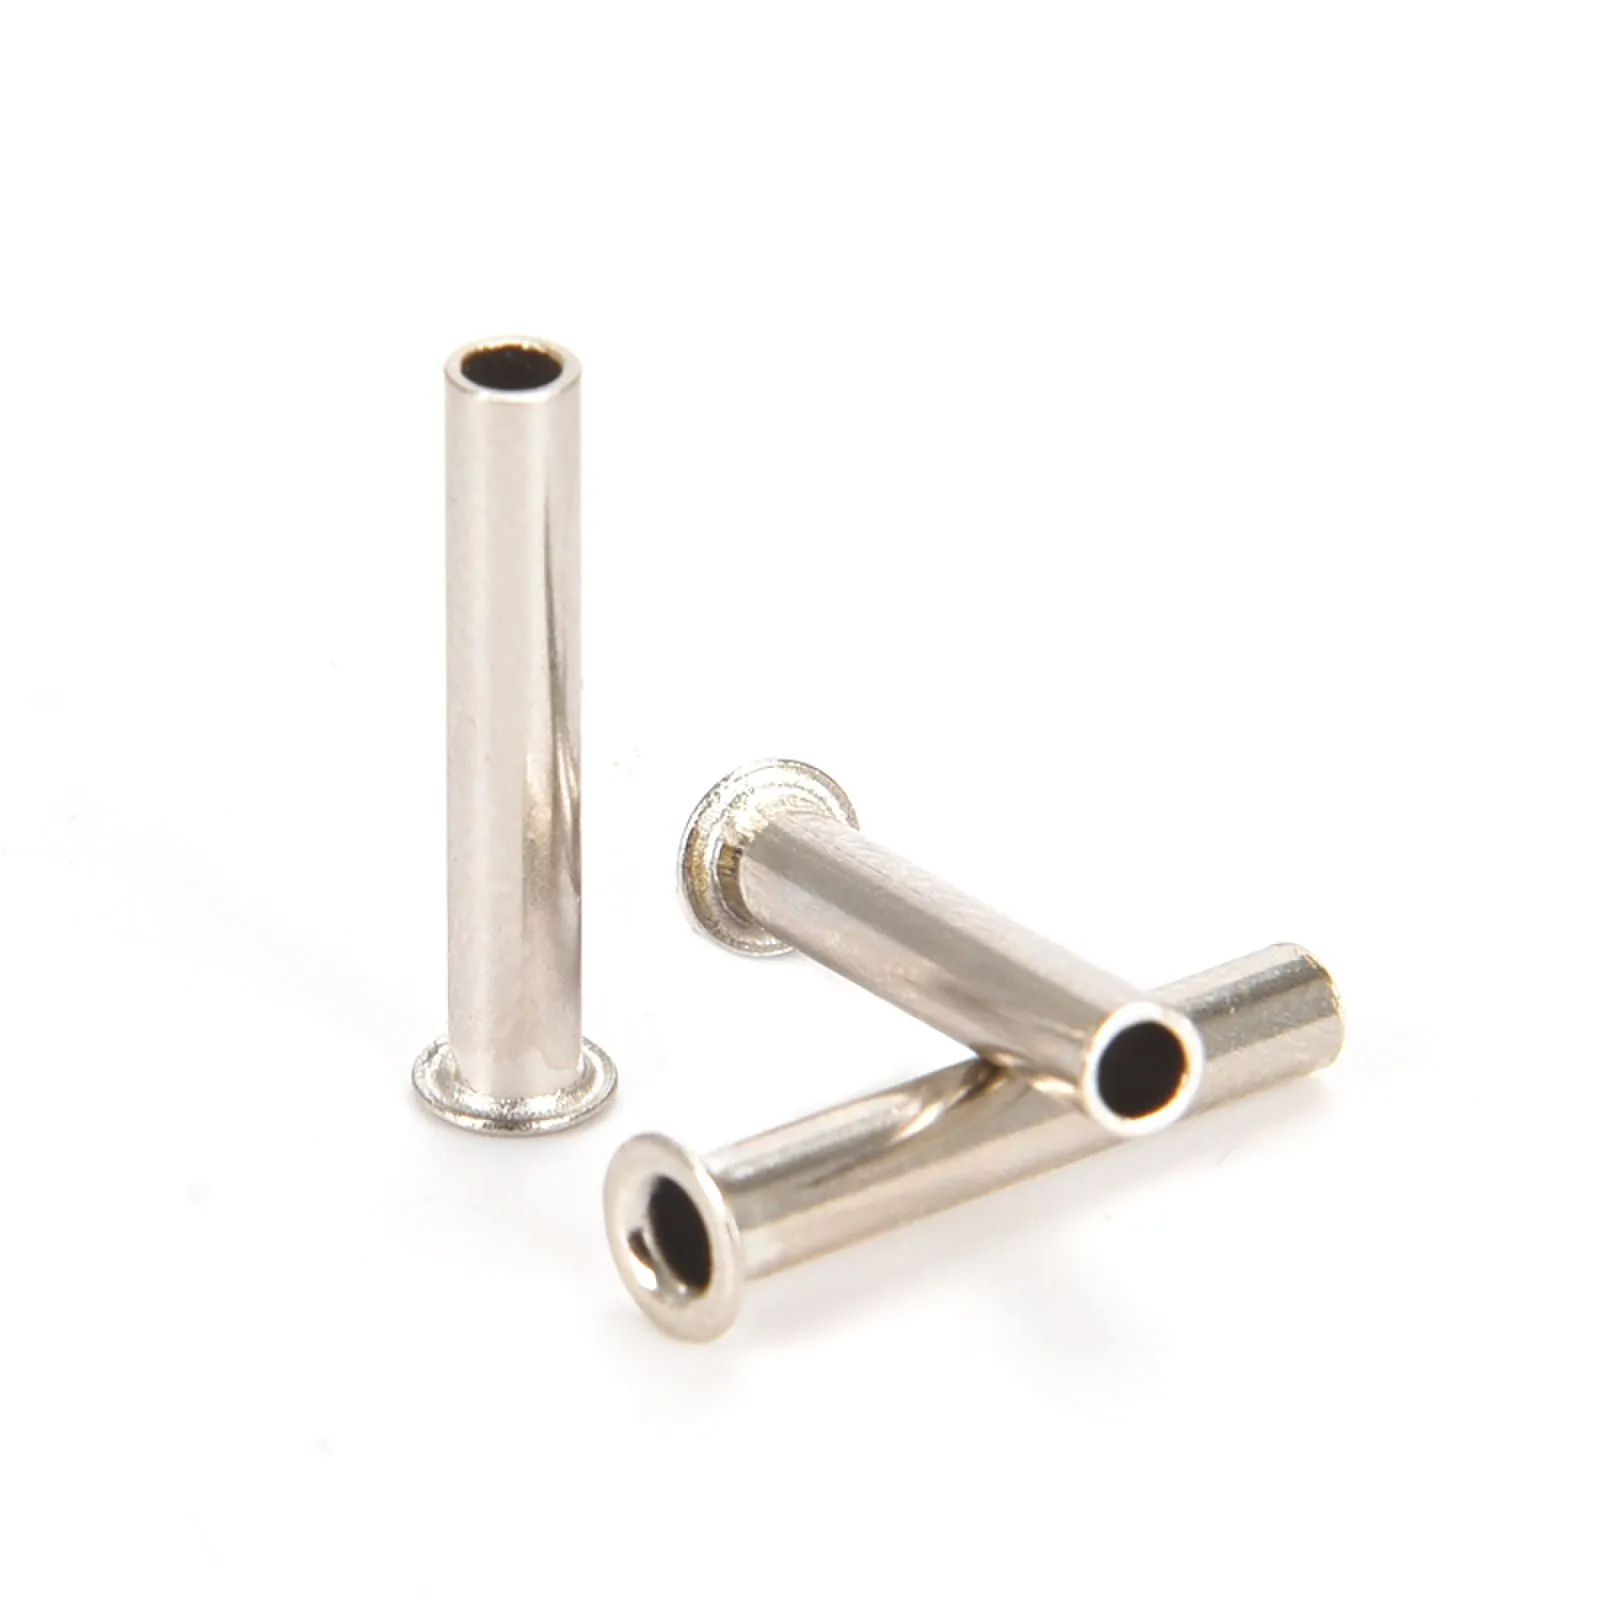
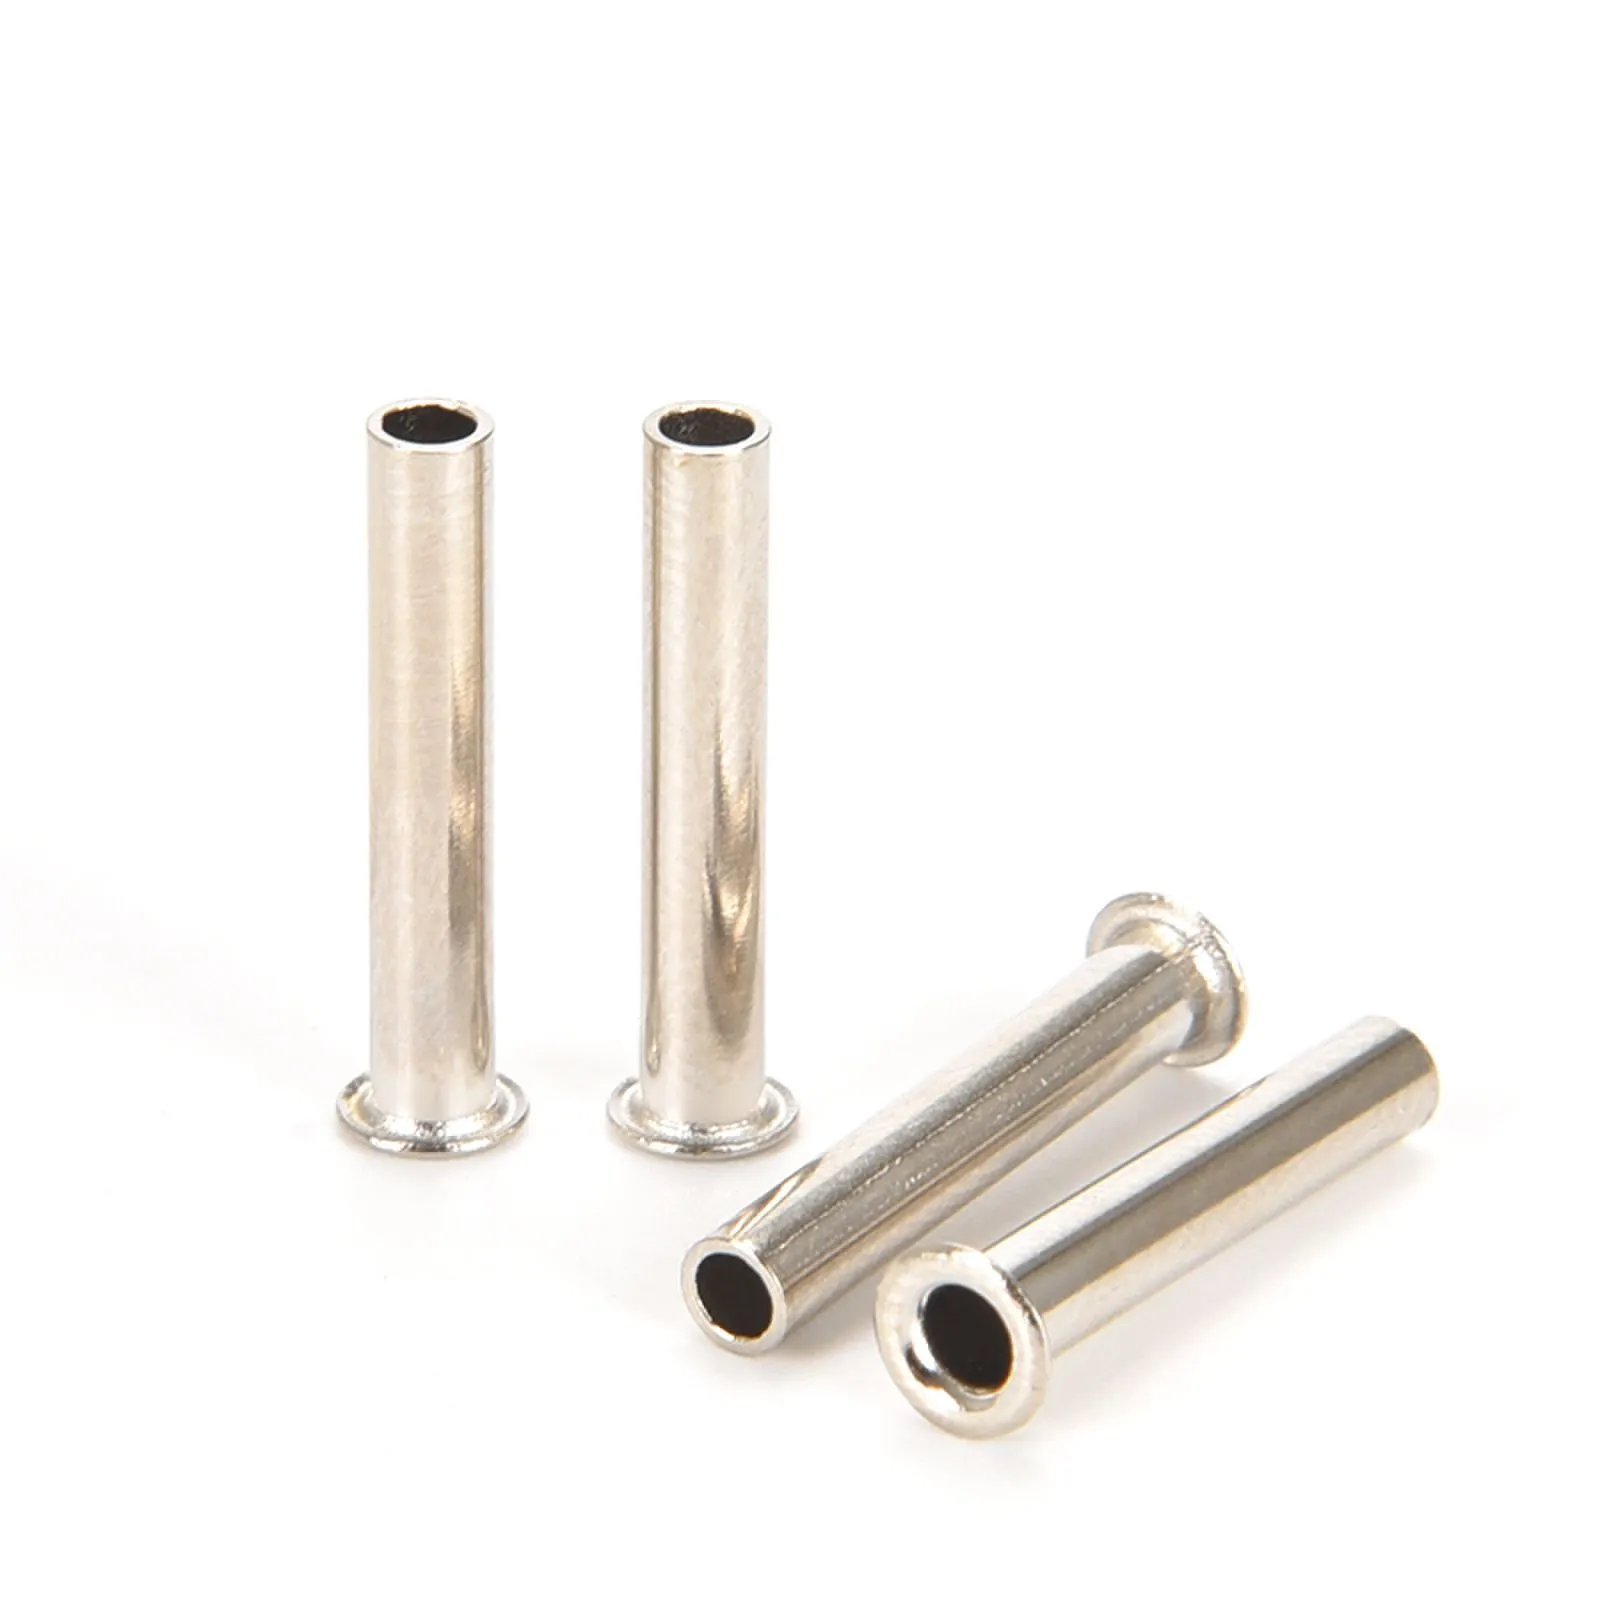
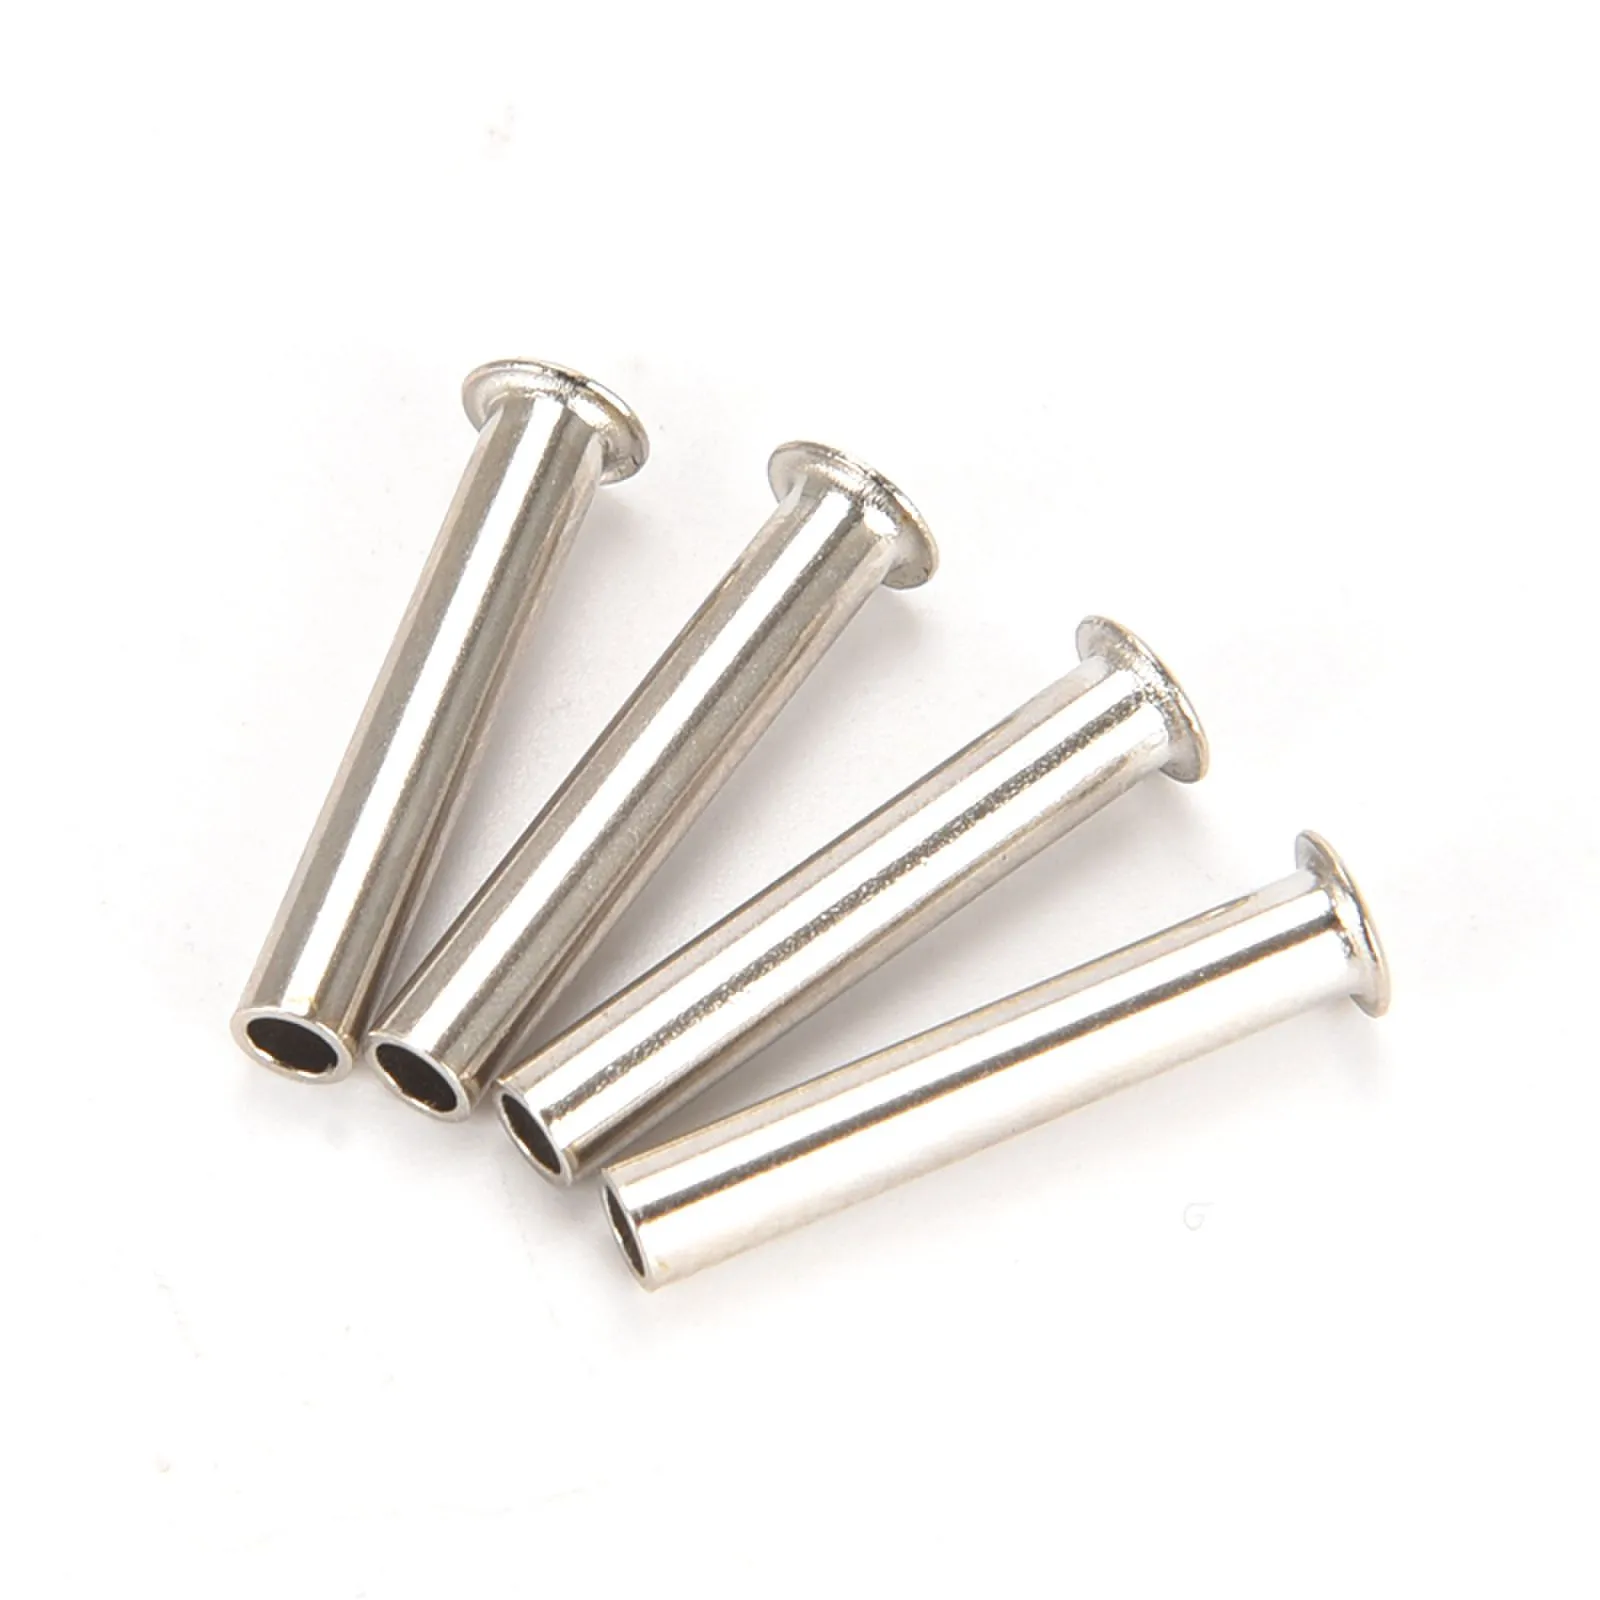
Stainless steel tubular rivets use an open hollow body and a formed head to create a lightweight joint with a visible bore. The gallery shows straight tubular parts with a flared or headed end, sometimes as single samples and sometimes in small groups. The open bore is the defining feature: it changes how the joint is designed, inspected and finished compared with a solid or semi-tubular rivet.
Head, wall and bore
The gallery shows several lengths and viewing angles, but it does not give a wall thickness or a bore tolerance. Those details should be taken from the drawing. If the bore is intended to remain clear after installation, state that requirement explicitly and identify any feature that could close or distort it.
Where tubular rivets are considered
Typical uses include hinges, pivots, lightweight fastening, decorative joints and assemblies that need an open passage through the fastener. They can also serve as a simple sleeve or pivot body when the surrounding design provides the retention. The application should identify whether the rivet carries shear, tension, a moving load or mainly holds parts in alignment.
A tubular rivet is not automatically a low-load part. The joint behavior depends on the head support, wall section, hole fit and installation method. For a hinge or pivot, check the bearing length and the clearance between the bore and the pin or shaft that will pass through it.
Stainless steel needs a grade and finish
Also confirm whether the bore and the head are supplied with the same finish. A process intended to improve the outside appearance can leave a burr or a change in dimension inside a small bore. State which surfaces are functional and which are visible.
How to specify a stainless tubular rivet
- Dimension the head profile, outside diameter, bore diameter and overall length.
- State the wall thickness, bore tolerance and whether the bore must remain open after setting.
- Identify the workpiece materials, hole fit, load direction and installation method.
- Specify the stainless grade, finish, passivation, inspection and quantity.
Inspection and trial assembly
Check the bore for burrs, debris and ovality. Inspect the head for cracks or a sharp edge that could damage the workpiece. Verify that the tubular body is straight enough to enter the hole without forcing. If the rivet will be flared or otherwise formed during installation, inspect a trial part after forming rather than relying only on the incoming dimensions.
In the assembly, confirm that the head seats, the tube reaches the intended depth and the bore remains usable. Check for movement between the joined parts and for any deformation that could affect a later pin or shaft. Keep the installation sample as the reference for the production inspection plan.
FAQ
Is a tubular rivet the same as a semi-tubular rivet?
No. A tubular rivet has an open bore through the body. A semi-tubular rivet has a different end configuration and setting behavior. Confirm the drawing rather than using the terms interchangeably.
Can a pin pass through the finished rivet?
That depends on the bore size, straightness and the amount of deformation during setting. State the pin diameter and the required clearance if the bore is a functional passage.
Which stainless grade should be used?
The grade depends on the service environment, mating materials and drawing requirements. Provide those details so the grade and finish can be selected and verified.
Browse the stainless steel tubular rivet category, or compare copper hollow rivets and internally threaded copper rivets.